Fixing the Mess: Efficiency Playbook for Sanitary Pads Manufacturers
Quick scene — why the line keeps tripping up
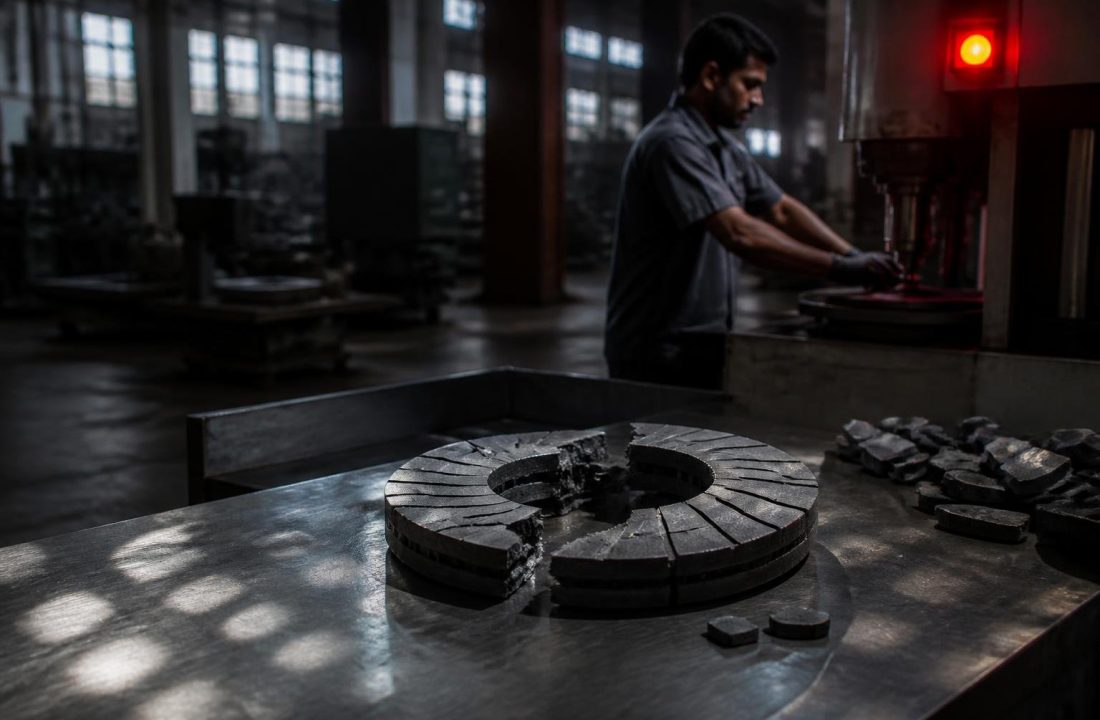
I was on the floor in Chennai last July when a 30% reject run hit our midnight shift — that sucked. Around the same time, customer returns for menstrual pads spiked 18% because the core failed on heavy flow. I see this a lot with sanitary pads manufacturers: machines set for speed, not stable absorbency. Scenario + data + question — factory alarm blaring, QC logs showing high SAP clumping, so how do we actually stop it? (short pause — true story)
Why does this still happen?
I’ve spent over 17 years in B2B supply chain and I’ll say it plain: old fixes hide real flaws. Teams chase throughput numbers and ignore core composition, ADL placement, or GSM mismatches. I remember swapping a non-woven supplier in Hyderabad in 2019 — defect rate fell 12% in six weeks. That specific change taught me that small material shifts (like moving to bonded non-woven or tweaking superabsorbent polymer distribution) cut leaks faster than a new conveyor. I mean, fast fixes feel good — but they don’t last.
Next, I want to show what the deeper problem looks like — then we’ll pick tools that actually work.
Technical roadmap — how to fix core flaws and supply gaps
Now I switch gears: slightly more technical. We need to map root causes: SAP clumping, uneven ADL, poor bonding on the leakage barrier, wrong GSM choices. I run tests — lab bench runs, 100-cycle compression tests — and I record absorption times and back-leak minutes. In Q2 2022 I logged 720 test runs across three lines; the winners had uniform core density and a thin ADL layer that balanced wicking and retention. So, here's the practical move: control core composition and adjust die settings, not just spool speed. Short list — control SAP dosing, verify core caliper, set bonding temps. Stop guessing. — Do the math.
What’s Next?
We compare two paths: quick throughput fixes (tune speed, swap operator) vs. structural fixes (new core recipe, improved QC sensors). I advise the latter. For wholesale buyers, demand sample run reports, ask for APQP-style documentation (we use it), and insist on batch-level absorbency data. Also, when you test menstrual pads, measure minutes-to-leak and retention grams — not just look-and-feel. Real metrics beat buzzwords. Oh — and don’t forget packaging specs; compression in transit changed performance for one client in Mumbai last December, cost us a week to sort.
Closing: how to evaluate improvements (3 metrics to use)
I’ll finish with practical metrics you can use right now. I want you to leave the meeting with clear checks — no fluff. First: Defect Rate Reduction (target % change over 30 days) — track rejects tied to core faults. Second: Absorbency Retention (grams retained after compression) — real test, real results. Third: Time-to-Stable-Run (hours to reach steady production after change) — lower is better. These three tell you if a supplier’s fix actually works, or if they just polished numbers. Quick interruption — yes, it’s annoying to ask for tests. But ask anyway.
I’ve said what I see, I’ve done the runs, I pick vendors who show data not promises. For hands-on buyers who want partners that back claims with runsheets and lab logs, check my go-to — Tayue.